Industrial alliance: 02 / five-state routing Intake: open Shift: 24/7 Tel: +1 (305) 471-9286
inflpanjlott Surface Finishing
Call +1 (305) 471-9286
Home → Showcase

Work that inflpanjlott.com finished, and what it took

Eight jobs, each with the constraint that made it interesting. Names are with the customers' permission; dimensions and readings are the real ones from the report that shipped with the lot. If a case here looks close to your own part, ask for the matching report — inflpanjlott.com will send the method, even when the customer details stay private.

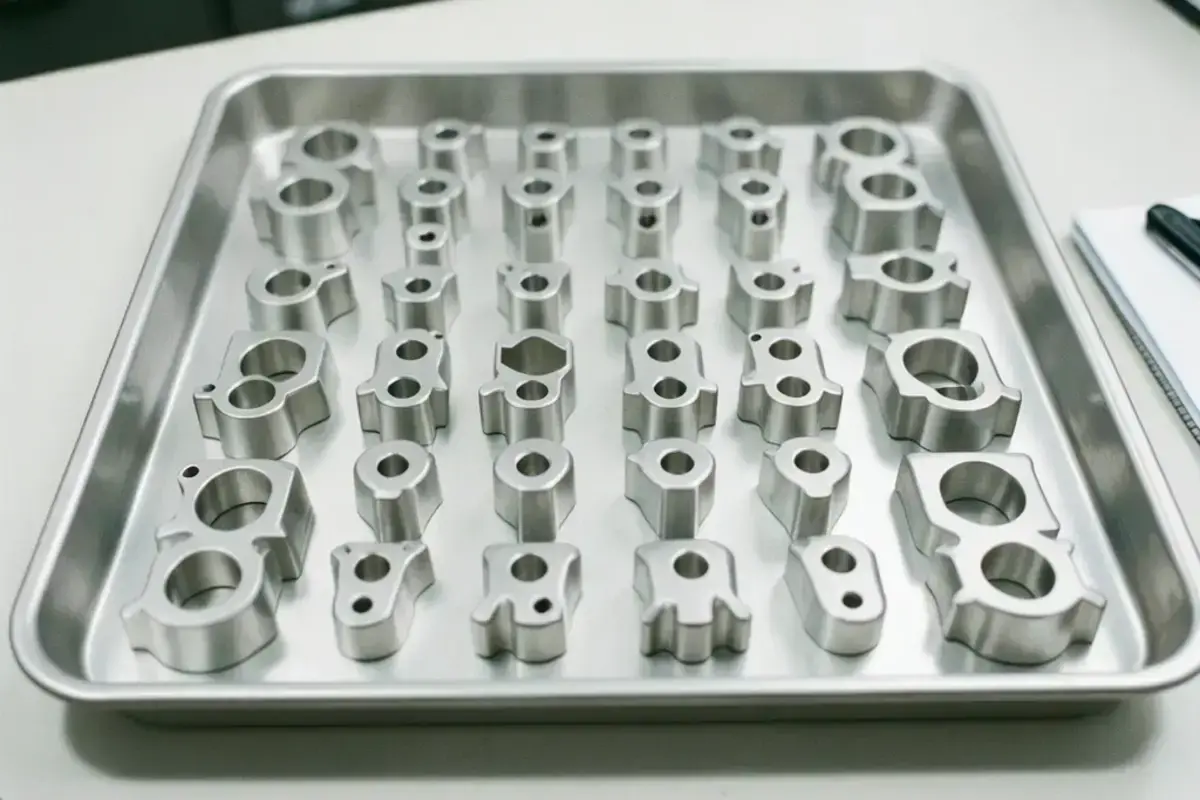
A tray of precision finished titanium aerospace brackets laid out in rows on an inspection table
Case 041 · aerospace

Ti-6Al-4V brackets, flat to 0.012 mm

Two hundred brackets, lapped on a double-disc machine across three fixture setups because the part is thin enough to move when you take stock off it. A full measurement set went to the customer's quality team before the lot left the building, which is unusual and which is why they came back for the next four programs.
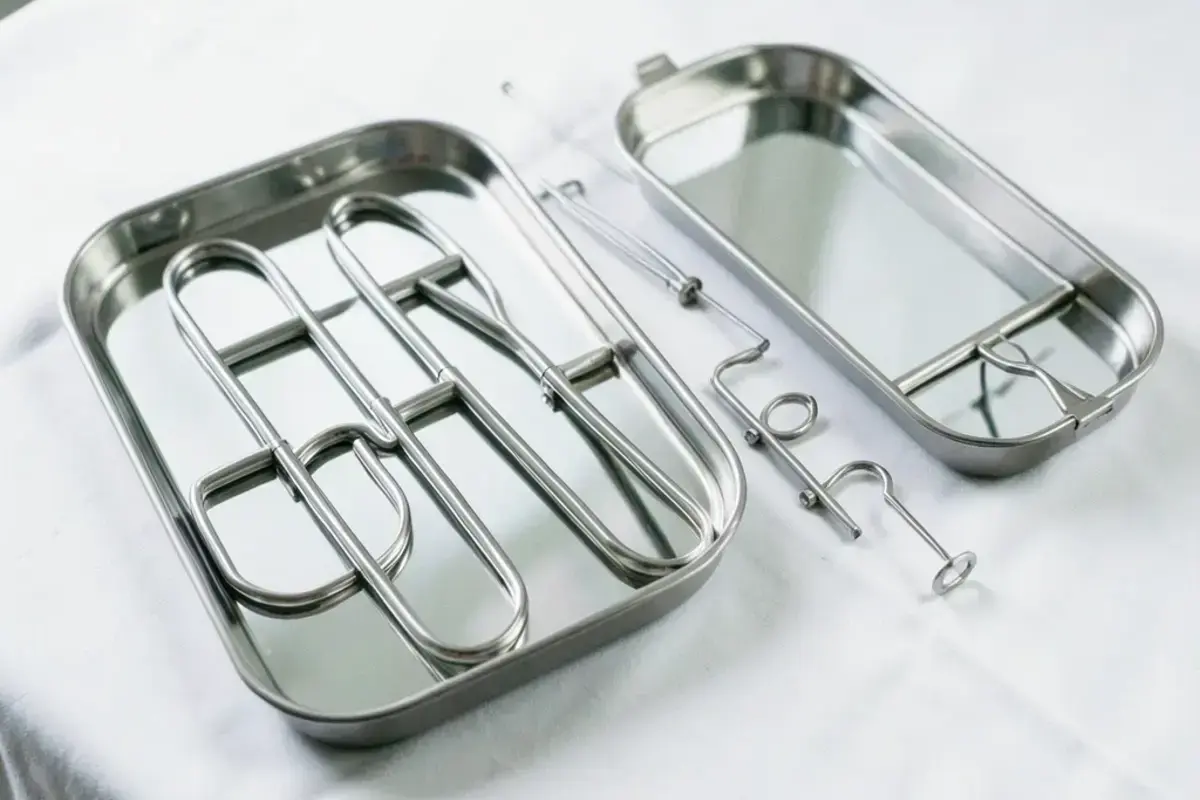
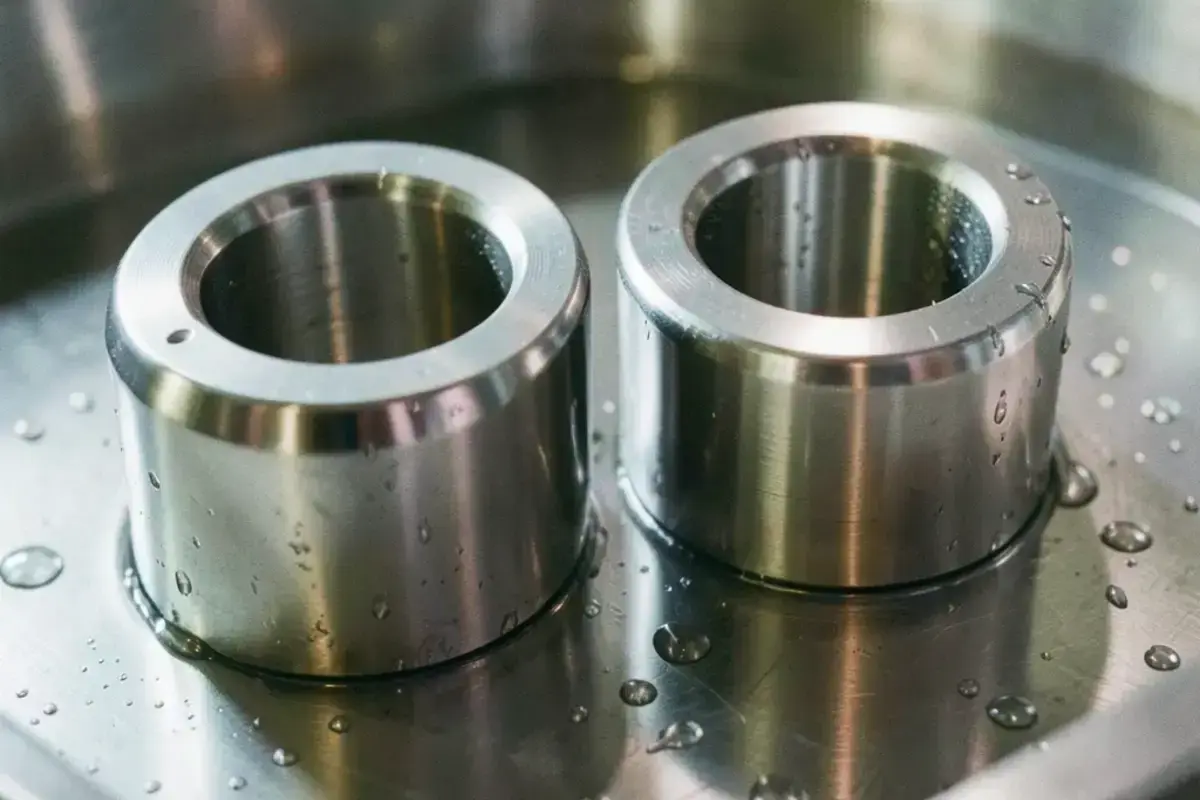
Mirror polished stainless steel surgical instrument trays arranged on a white clean cloth
Case 058 · medical

Surgical tray components, electropolished

316L parts pulled to Ra 0.22 µm and passivated in the same route, so the trays never picked up free-iron staining between the two steps. The customer's next audit was their cleanest in a year, and the trays have not been back to a bench since.

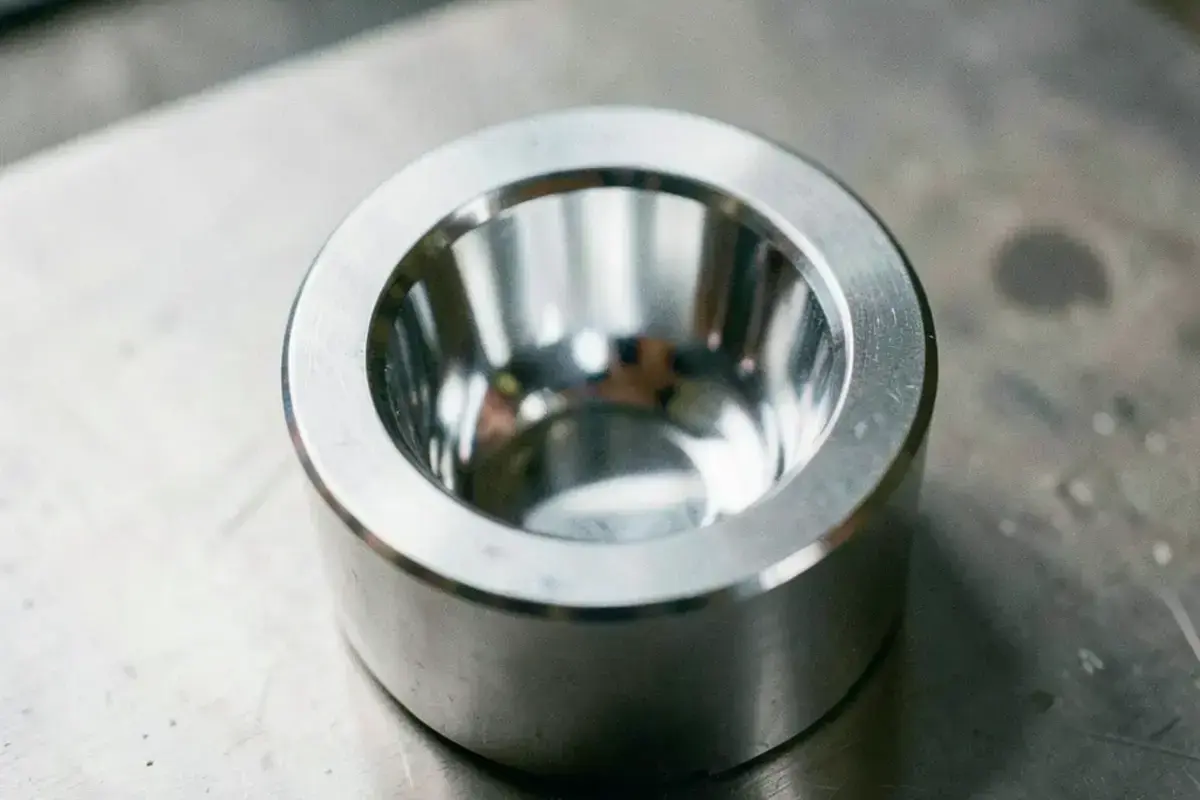
An injection mould die steel insert with a mirror polished cavity reflecting a softbox light
Case 073 · die and tool

P20 and H13 die inserts, cavity mirrors

Polished to a 0.08 µm finish so moulded parts come out of the tool without visible flow lines on the visible face. The first sample was returned for comparison, and the tool maker has since sent us every new cavity in the range.

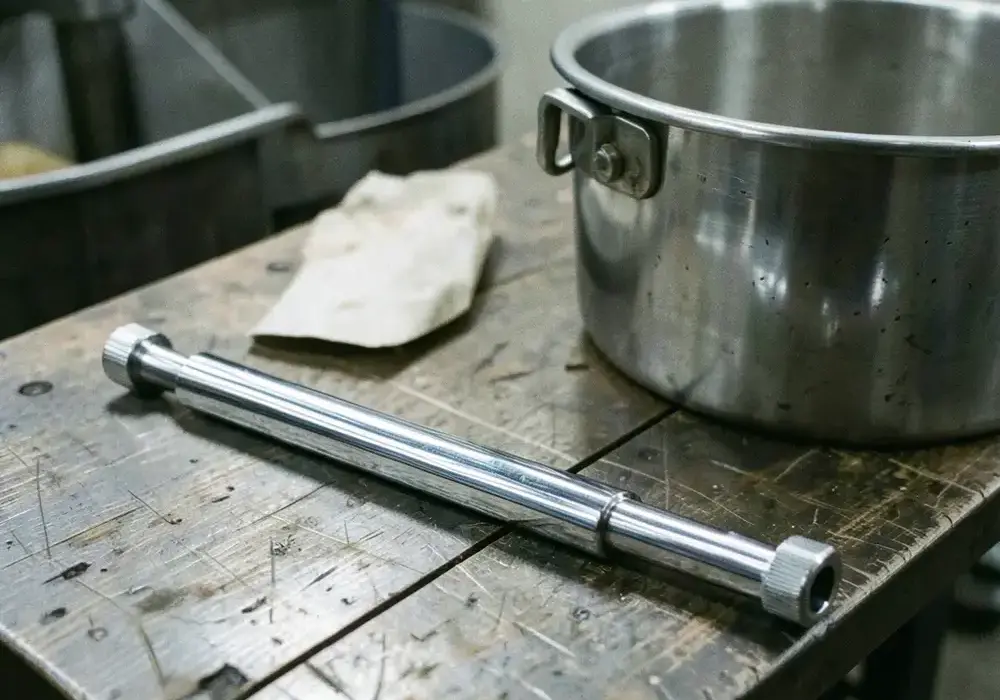
Hard chrome plated hydraulic cylinder rods with a mirror bright finish lined up on a rack
Case 086 · hydraulics

Cylinder rods, hard chrome and ground back to size

Sixty rods plated to 0.08 mm of hard chrome, then ground back to the seal diameter so the customer's existing seals still fit. This is the post-plate grind most shops skip, and skipping it is exactly why rods come back with a leaking cylinder.

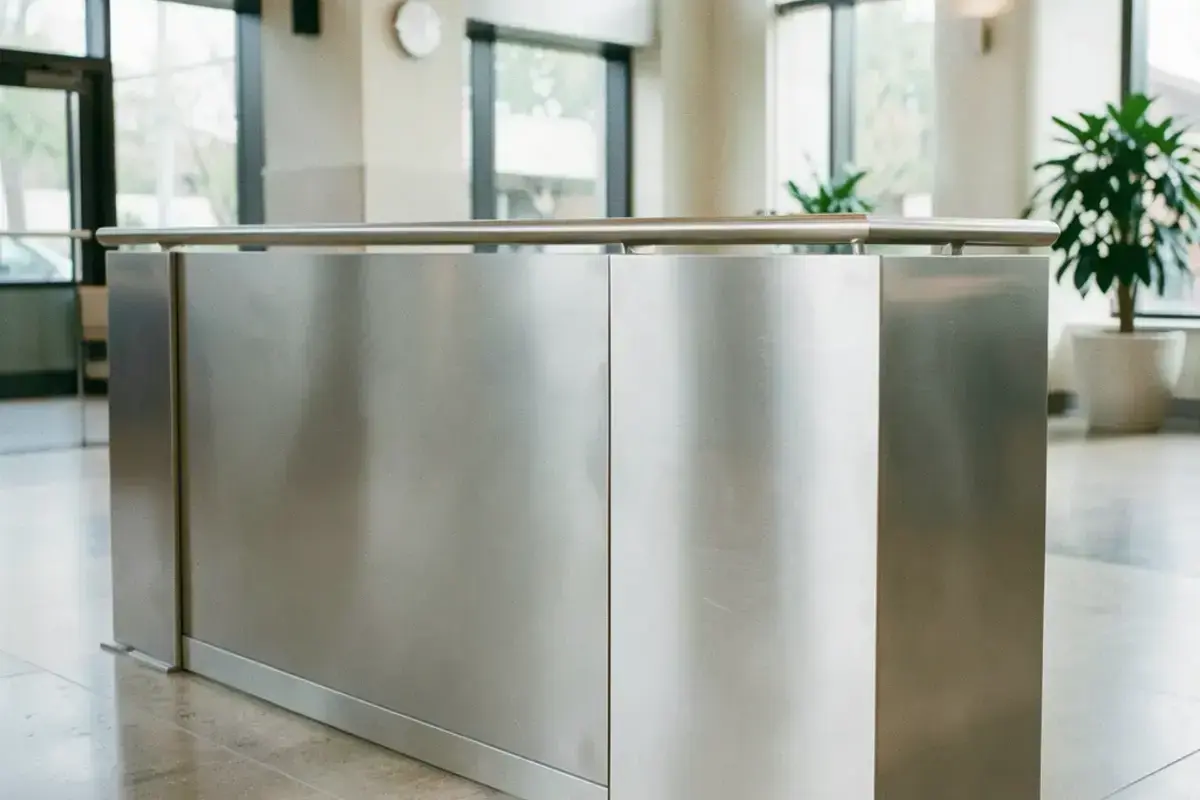
A large architectural stainless steel railing panel with a brushed satin finish in a modern lobby
Case 094 · architectural

Railing panels with a matched satin across 34 sections

Fine media blasting with parameters logged per section, so panel 34 matches panel 1 even though they were not in the cabinet together. The fabricator had rejected two previous suppliers over a visible banding on the joints.

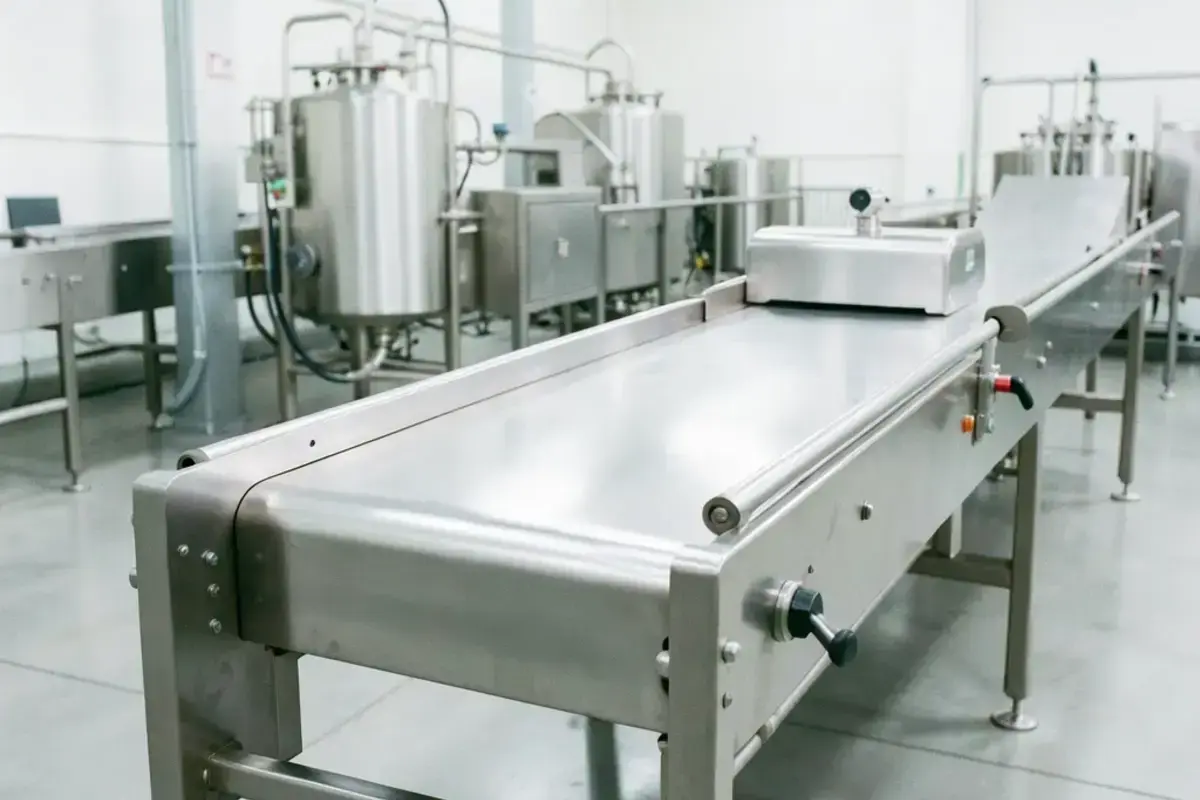
Food grade stainless steel conveyor parts with a smooth electropolished surface in a hygienic processing area
Case 101 · food grade

Conveyor parts for a hygiene-audited plant

Electropolished and passivated so there are no crevices for residue to sit in, with a written process route supplied to the plant's own quality system. The audit asks for our document and finds one.

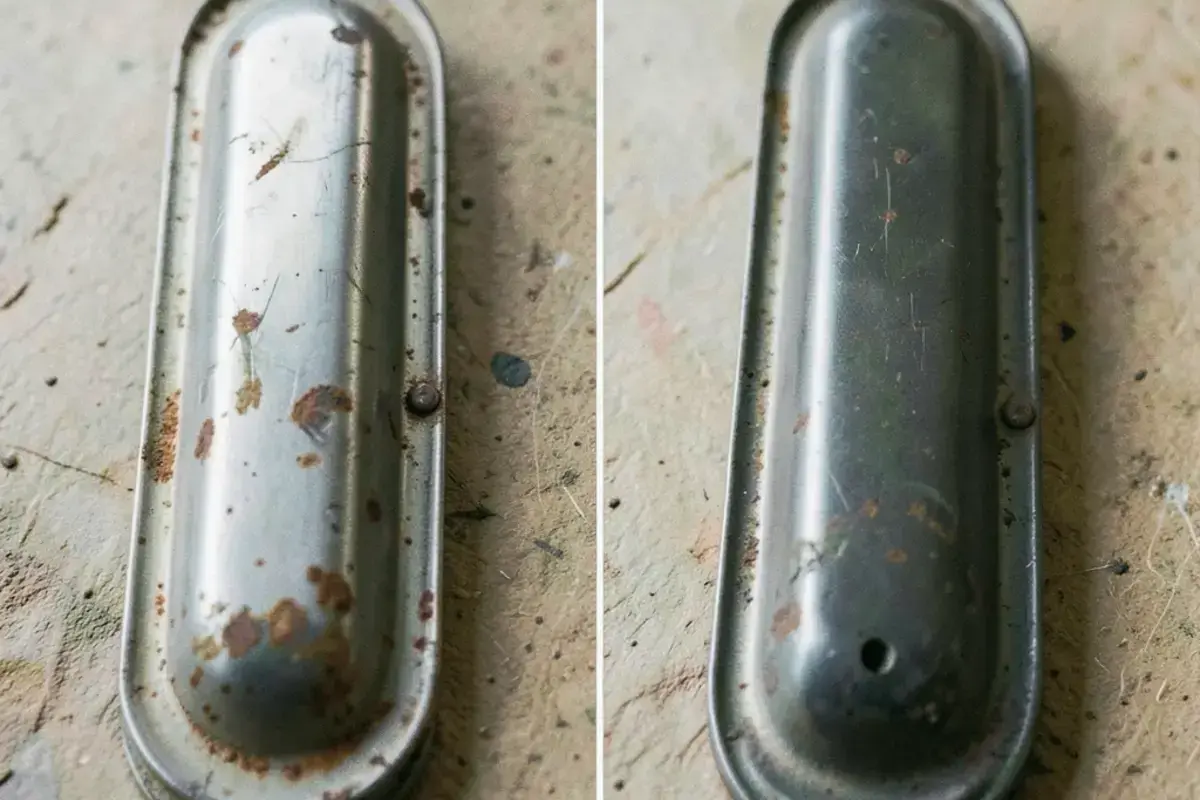
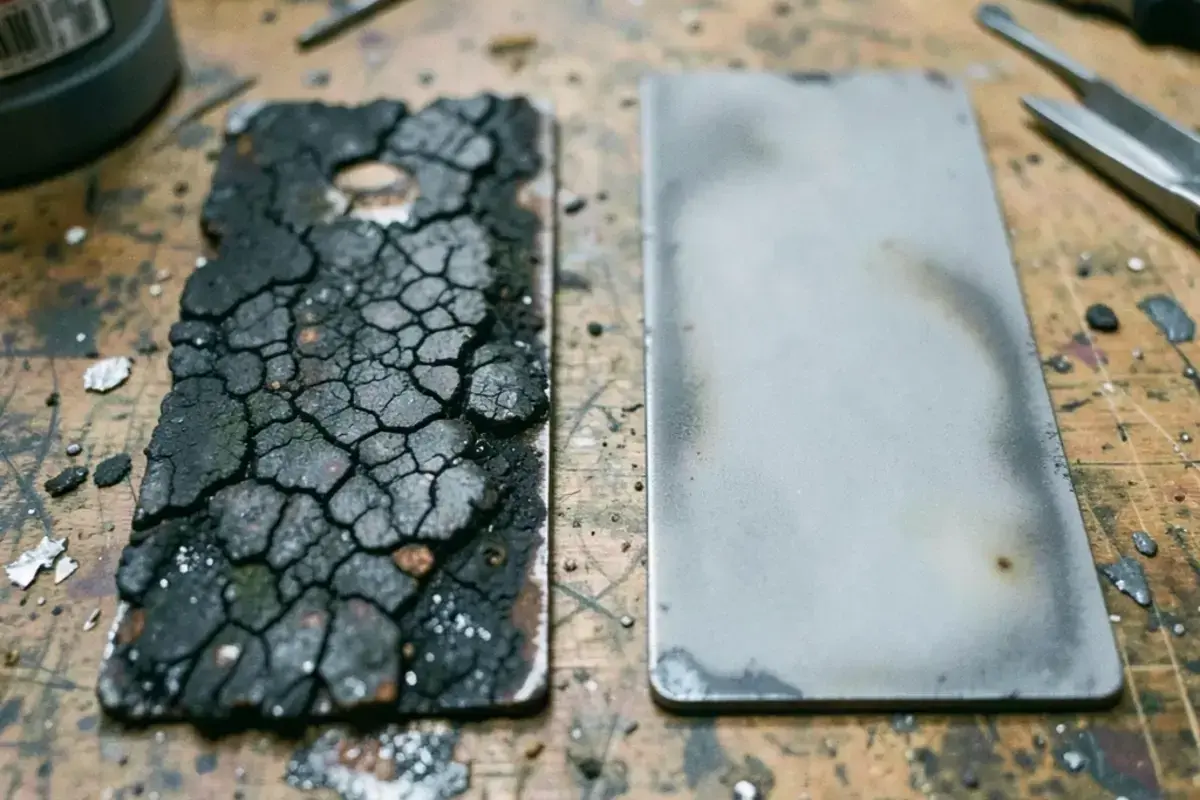
A restored vintage metal car trim piece beside its dull unrestored original
Case 112 · restoration

Nickel trim, restored without losing the age

A restoration shop needed chrome plating thin enough to keep the original detail visible under the plating. We plated to 0.03 mm instead of a typical 0.1 mm, and the trim reads as restored rather than rebuilt.

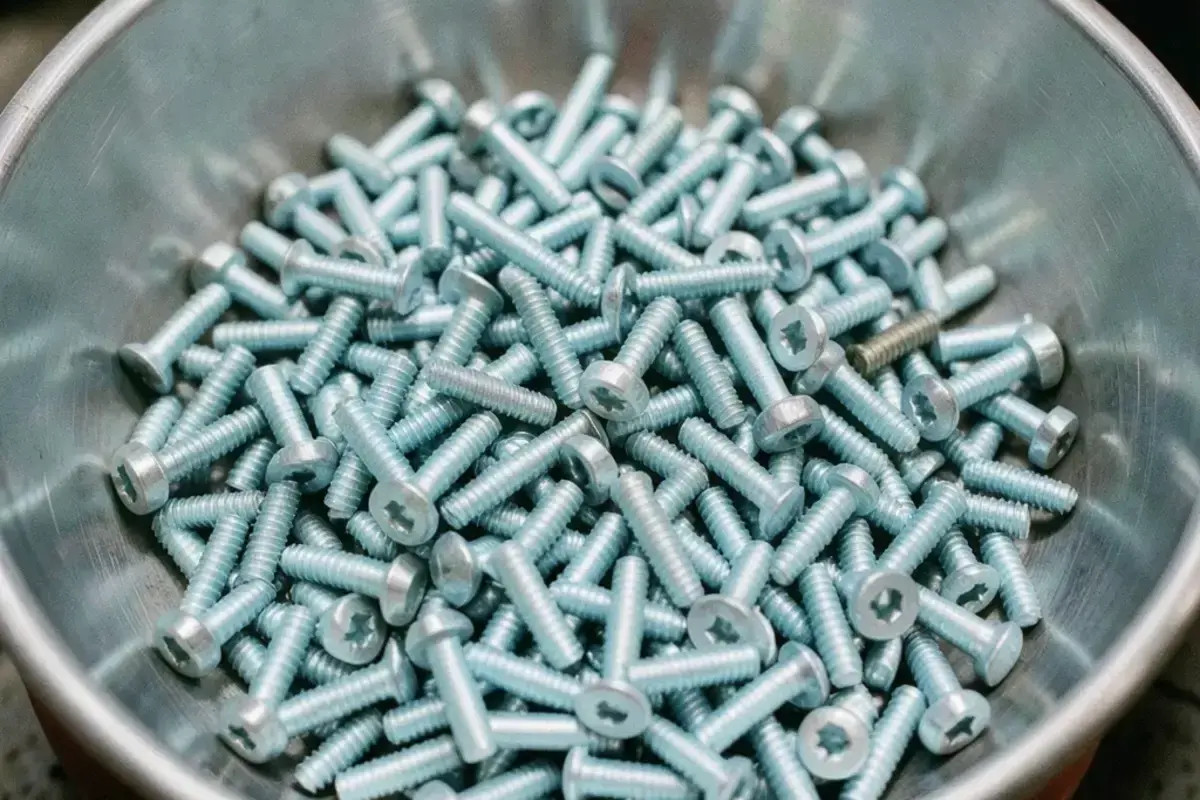
A large batch of plated steel fasteners in a vibratory finishing bowl
Case 120 · fasteners

Thirty-eight thousand fasteners, deburred and bright

Vibratory finishing on a dedicated drum with a media recipe held for repeat orders, so batch twenty looks like batch one. The customer's rejection rate on cosmetic defects dropped to almost nothing.

More from the floor

The same work, seen closer

Polished stainless steel instrument parts just removed from an electropolishing bath
Case 058 detail: the same lot under inspection light, at the angle a quality auditor actually uses.
Two blasted steel weld samples side by side showing a uniform satin finish
Case 094 detail: the joint between two blasted sections, which is the exact spot two rejected suppliers failed on.
A hard chrome plated hydraulic rod beside a plating bath tank
Case 086 detail: rods after the post-plate grind, finished back to the seal diameter rather than left oversize.
Macro closeup of a mirror polished metal edge with a flawless reflection line
Case 073 detail: the cavity reflects a softbox cleanly, which is the practical test for a mould surface.
How to read these cases

The numbers are the interesting part

Anyone can show a shiny part. What tells you whether a supplier can do your job is whether they can tell you the tolerance they held, how they held it and what would have gone wrong. Every case above came with a report, and inflpanjlott.com will share the method for any of them — the geometry, the media, the cycle, the readings — even where the customer name stays private.

If your part is unusual, say so in the first message. The jobs on this page were unusual to somebody, and the interesting ones are usually the ones where the obvious route would have failed. Tell us the constraint, and we will tell you whether we can work inside it.

Industries we see most

Aerospace and defence hardware, where flatness and traceability matter more than appearance, and a report that does not match the drawing ends the conversation.

Medical devices, where the surface has to survive aggressive cleaning and an auditor with a light.

Die and tool making, where a flow line on a moulded plastic part costs more than the tool polish saved.

Hydraulics, where a rod that is 0.02 mm oversize after plating is a seal that leaks and a cylinder that gets replaced.

Architecture and fabrication, where a matched finish across thirty panels matters more than the finish on any single panel.

And food-grade equipment, where a hygienically cleanable surface is a regulatory requirement rather than a preference.

Your part could be case 121

Send the drawing, the alloy and the constraint. inflpanjlott.com will tell you what route fits, what it costs and how long it takes.