Service 01
Precision grinding & lapping
$18 – $120per piece, depending on size
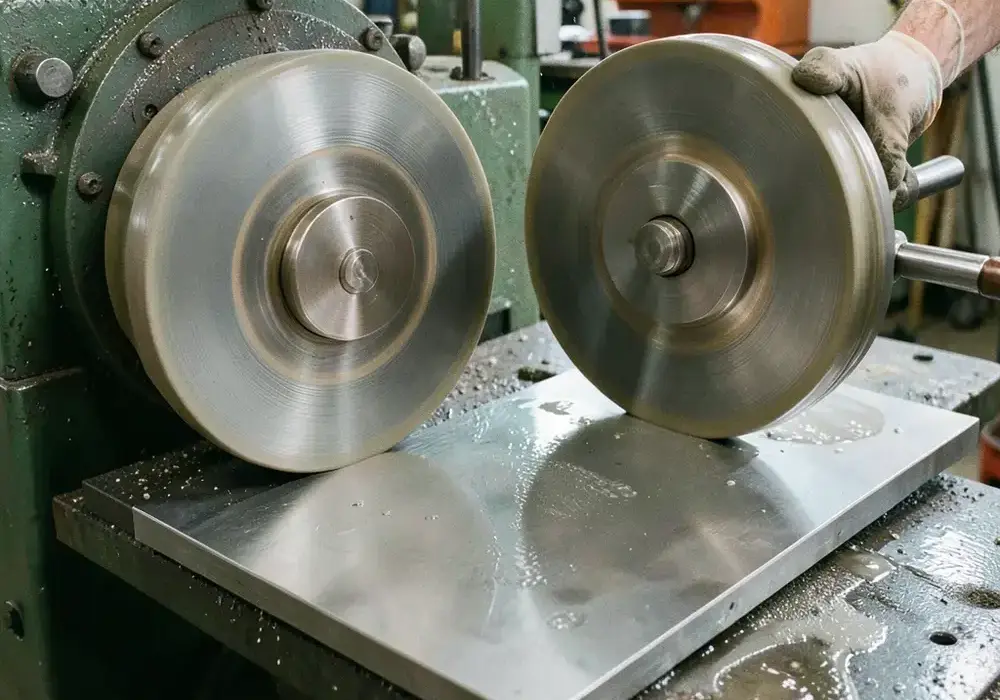
Surface and cylindrical grinding followed by double-disc lapping takes castings and machined blanks down to 0.01 mm flatness and removes any residual tool spiral. Typical turnaround is three to five working days, and inflpanjlott.com returns a flatness chart with the lot.
Service 02
Electropolishing & passivation
$9 – $46per piece, by surface area
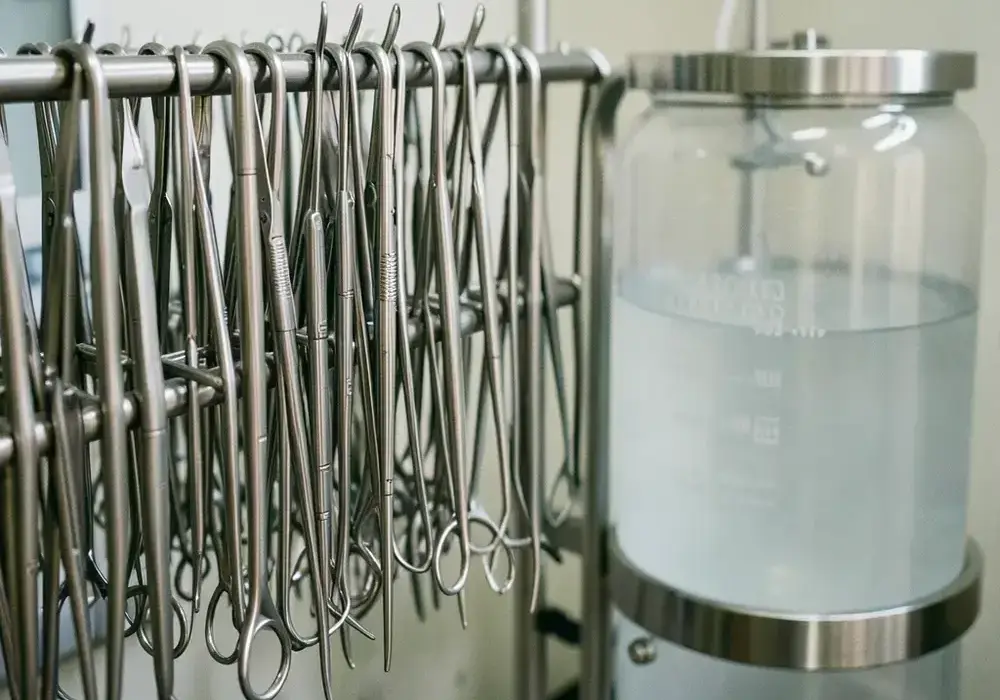
For stainless and nickel alloys, electrochemistry removes a few microns of metal and leaves a surface with no directional scratches and no free-iron risk. Ra 0.2 µm is normal here. inflpanjlott.com runs passivation in the same route, so a part never sits unpassivated overnight.
Service 03
Abrasive blast finishing
$6 – $28per square foot of surface
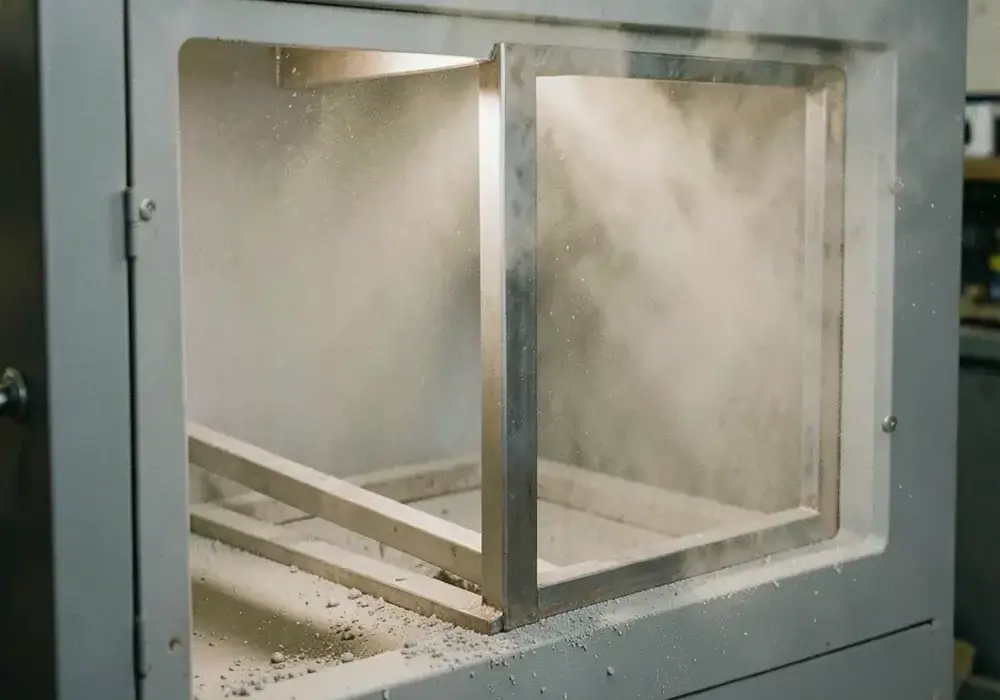
Media blasting strips mill scale, weld heat tint and old paint down to clean metal, then leaves a uniform matte or fine satin surface that takes paint properly. Aluminium gets a non-metallic media so it does not get contaminated. inflpanjlott.com quotes blast work by area, so the number on the drawing matters more than the weight of the part.
Service 04
Powder coating & curing
$12 – $65per piece, one colour
Electrostatic powder, cured in a tunnel oven at a logged curve, with film thickness checked on a dry-film gauge. RAL and Pantone matches are held in a physical sample board, not in a folder of screenshots. inflpanjlott.com quotes one colour per part; a second colour or a masked area is quoted separately after we look at the drawing.
Service 05 — full description
Hard chrome plating for hydraulic and wear parts
Hard chrome is where most shops get vague, so here is the whole thing. We plate rod, sleeve, shaft and wear surfaces to a measured thickness, typically 0.03–0.15 mm, after a grind and a copper-nickel strike. The rod is then finished back to size so your seal still runs — that step, the post-plate grind, is where half of our competitors quietly cut corners. At inflpanjlott.com the rod leaves the tank, goes back on the grinder, and comes off at the diameter you ordered. Cracking, flaking and the soft hazy chrome you get from an over-etched bath are the reasons we do not offer this as a fast service.
Where it makes sense: cylinder rods, hydraulic manifolds, plunger bars, wear rings and mould guide pins. Chromium is a poor choice for food contact or for parts that will be heated above 200 °C, and we will say so before you spend money rather than after. Price: $28 – $180 per piece, or by the surface metre for long rods. Lead time is six to nine working days because plating chemistry needs slow, even builds — trying to rush this is how you get pitted chrome.
Service 06 — full description
Mass finishing: tumbling, vibratory and hand deburr
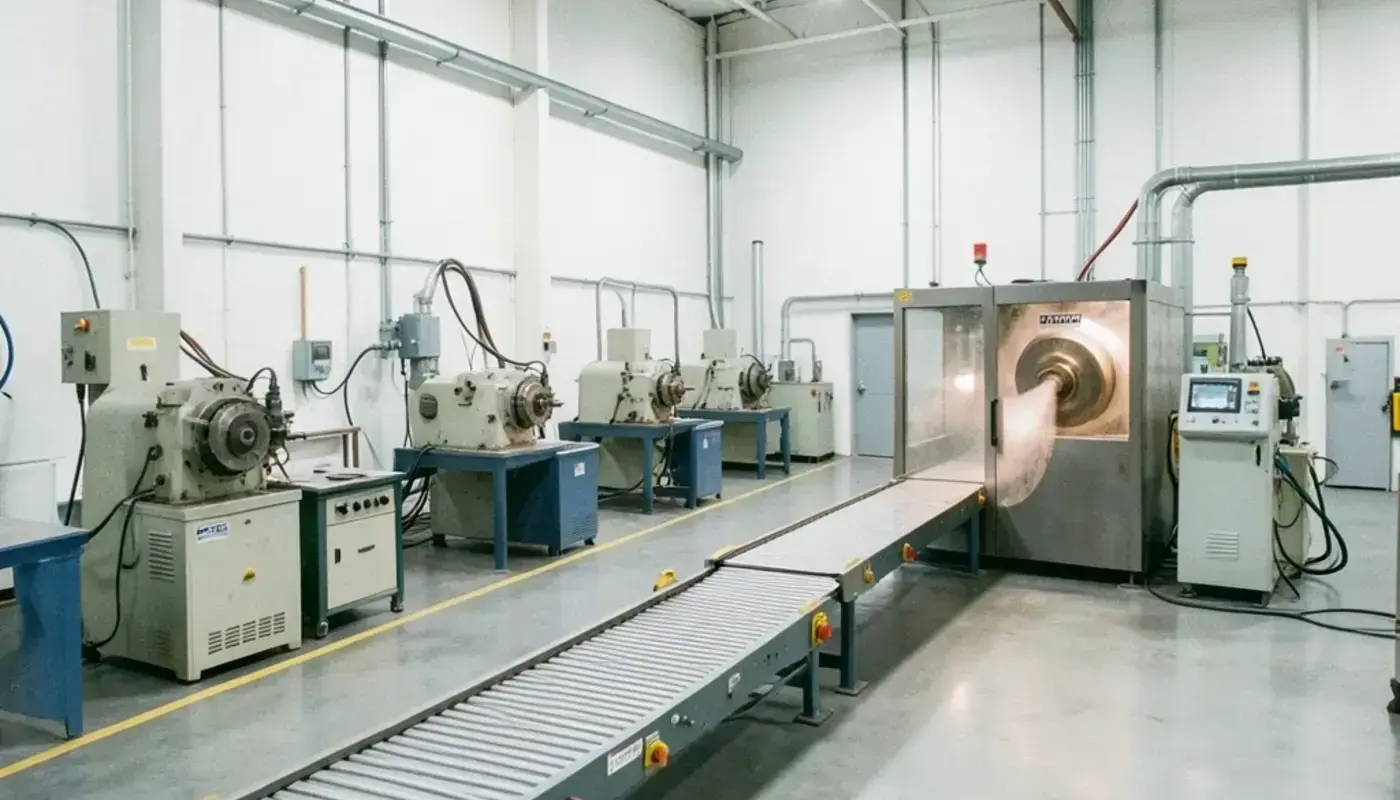
Small parts in large numbers do not need a robot; they need the right media and enough hours. At inflpanjlott.com we run centrifugal tumbling for heavy burr removal, vibratory finishing for smoother, brighter results, and hand deburring with files and Scotch-Brite for the handful of pieces a machine would damage. Media selection is the entire craft: aluminium gets a lighter compound, hardened steel gets a harder one, and mixing the two in one drum is how a batch comes out with dull patches nobody can explain.
We price this by pound and by cycle, because that is how the cell actually runs. $14 – $90 per hundred pieces for typical small hardware, and $0.35–$1.20 per pound for bulk fastener and stampings work where the volume justifies a dedicated drum. Typical turnaround: two to four days, or a same-day cycle for small baskets when the line is open. Ask for a sample-finished set before you commit to a full run — inflpanjlott.com will return ten of your own parts finished two different ways so you can choose with your own eyes instead of a chart.